Box Build Integration: Extending PCBA NPI to Full System Assembly
PCBA New Product Introduction traditionally focuses on the circuit board itself: component placement, soldering, and electrical test. Yet for many products, the PCBA is only one subsystem within a larger mechanical and electrical assembly. Cables, housings, displays, power supplies, and thermal management components must all integrate with the PCBA to create a finished product. When this box build integration is treated as an afterthought—handled by a separate vendor with no connection to the NPI services that validated the board—integration failures emerge: connector mismatches, cable routing interference, grounding issues, and thermal hotspots that were invisible during standalone PCBA test.
At 1943 Technology, box build integration is treated as a natural extension of PCBA New Product Introduction. Our turnkey PCBA capabilities extend beyond board-level assembly to full system integration, with NPI services methodologies applied to the complete product.
The Integration Gap in Traditional NPI
Traditional NPI services often conclude at the PCBA boundary. The board is electrically verified, packed in antistatic bags, and shipped to a separate integration house. This handoff creates several failure modes:
Mechanical Interference: A PCBA that passed all electrical tests may have tall capacitors or connectors that collide with the enclosure lid. A heatsink that cleared all components during board-level inspection may foul a cable harness in the integrated assembly.
Grounding and EMC: Standalone PCBA test cannot reveal grounding loop issues that only appear when the board is mounted in a metal chassis with multiple ground points. Electromagnetic compatibility (EMC) violations often trace to integration-level grounding errors rather than board-level design flaws.
Thermal System Coupling: A board that operates within thermal limits on an open bench may overheat when enclosed, where natural convection is replaced by conductive and forced-air paths that depend on enclosure design.
Cable and Connector Mismatches: Pinout errors, connector keying mismatches, and cable length inadequacies are integration-level defects that board-level NPI services cannot catch.
System-Level Design Validation
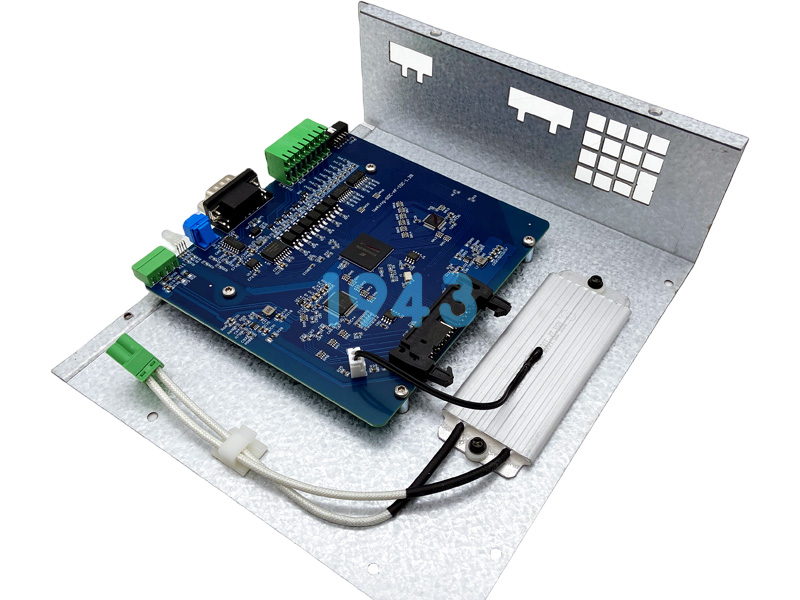
When 1943 Technology manages box build as part of PCBA New Product Introduction, design validation expands to include system-level considerations:
Enclosure Interface Review: The PCBA mounting holes, connector panel cutouts, and component keep-out zones are cross-checked against the mechanical enclosure drawings. Tolerance stack-up analysis confirms that worst-case dimensional variation still permits assembly.
Cable Routing and Strain Relief: Cable lengths, bend radii, and connector orientations are validated using physical mockups or 3D assembly models. Strain relief features are confirmed to prevent connector damage during handling.
Thermal Modeling and Validation: Computational fluid dynamics (CFD) or physical thermal mockups evaluate the integrated thermal path. If the enclosure restricts airflow, fan placement and venting are optimized during NPI services rather than discovered during pre-production builds.
Grounding and Shielding Strategy: The system grounding architecture is reviewed for single-point ground integrity, shielding effectiveness, and ESD discharge path compliance. This review prevents EMC test failures that would otherwise require costly redesign.
Box Build Process Validation
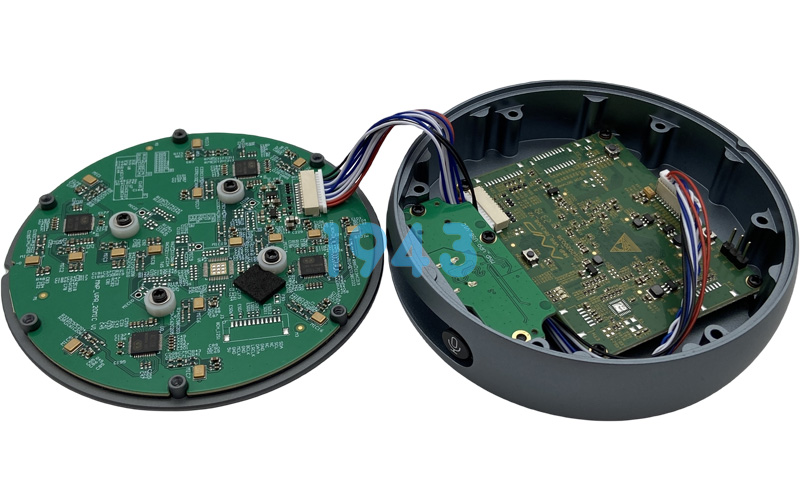
The assembly processes for box build differ significantly from SMT assembly. During process validation, 1943 Technology characterizes:
Mechanical Assembly Sequencing: The order of operations—PCBA insertion, screw fastening, cable connection, subassembly installation—is documented and validated for efficiency and ergonomics. Incorrect sequencing can damage fragile components or make later steps inaccessible.
Torque Specification Validation: Screw fastening torques are specified for electrical grounding integrity and mechanical retention. Over-torque cracks plastic bosses or strips threads; under-torque creates loose grounds. Torque validation during NPI services establishes the correct range and verifies it with calibrated torque wrenches.
Adhesive and Potting Processes: Some integrations require structural adhesives or potting compounds. Cure schedules, dispensing patterns, and material compatibility with PCBA coatings and labels are validated during pilot builds.
Labeling and Cosmetic Inspection: Final product labeling, including regulatory marks, serial numbers, and branding, is validated for placement accuracy, adhesion, and legibility. Cosmetic acceptance criteria are defined to prevent subjective judgment disputes during volume production.
System-Level Functional Test
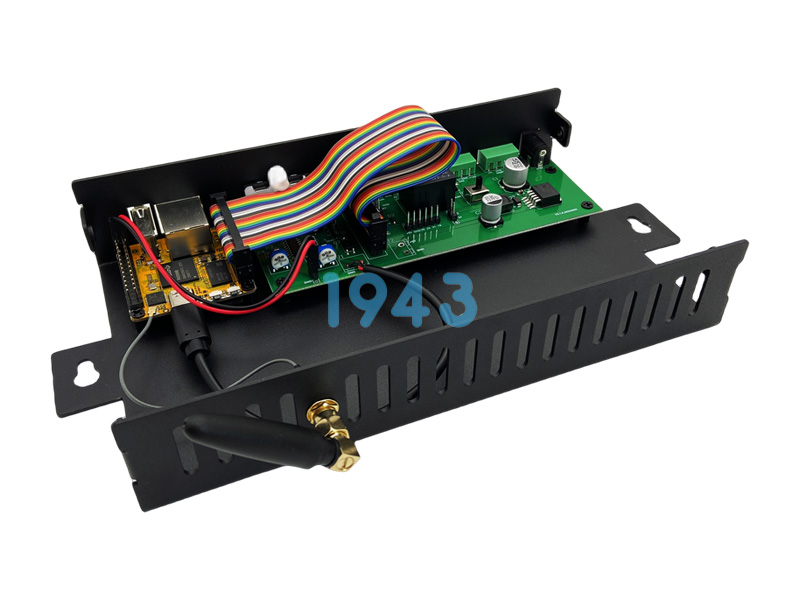
The FCT strategy for box build extends beyond PCBA electrical test to full system verification:
Power-On Self-Test (POST): The integrated product is powered on, and embedded diagnostics verify that all subsystems communicate correctly.
Communication Interface Test: If the product has external ports (USB, Ethernet, wireless), these are exercised with real or emulated counterparts to confirm protocol compliance and signal integrity.
Environmental Stress Screening: The integrated product may be subjected to temperature cycling, vibration, or altitude simulation during production validation to identify weak mechanical joints or cold solder joints that only appear under system-level stress.
Packaging Integrity Test: The final packaged product is subjected to drop, vibration, and compression testing to confirm that shipping stresses do not damage the integrated assembly.
Documentation and Supply Chain Consolidation
Box build NPI services produce a unified documentation set: PCBA manufacturing records, mechanical assembly instructions, system test procedures, and packaging specifications. For turnkey PCBA customers, this consolidation eliminates the need to coordinate multiple vendors. Quality responsibility rests with a single entity.
Supply chain management also consolidates. The BOM for a box build includes not only electronic components but also mechanical parts, cables, power supplies, and packaging materials. 1943 Technology manages this extended BOM under the same NPI services procurement discipline: supplier qualification, material validation, and inventory management.

Frequently Asked Questions
Q1: Does box build NPI require separate tooling from PCBA NPI?
A: Yes. Box build requires mechanical fixtures, torque tools, and potentially custom test jigs that differ from SMT assembly tooling. During NPI services, these tools are designed, fabricated, and validated in parallel with PCBA process development.
Q2: Can customers supply their own mechanical components for box build?
A: Yes. Customers may specify enclosure suppliers or provide proprietary mechanical parts. 1943 Technology integrates these customer-supplied items into the turnkey PCBA assembly flow, managing them with the same traceability standards as procured electronics.
Q3: How is system-level EMC testing handled during NPI?
A: 1943 Technology performs pre-compliance EMC screening during production validation using in-house or partner test facilities. Formal certification testing is typically customer-managed, but our NPI services output includes design guidance and grounding documentation to support certification.
Q4: Is box build integration suitable for very low volumes?
A: Box build integration is scalable. For low volumes, manual assembly with documented work instructions is employed. For higher volumes, semi-automated mechanical assembly and robotic fastening may be introduced. NPI services define the appropriate assembly mode based on volume forecasts.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08