Test Strategy in PCBA NPI: From Prototype Validation to Production Test
The test strategy in PCBA NPI decides how quickly you find out that a design works — and how much escapes into production. A strategy defined at the start of NPI catches defects at the cheapest stage; one invented after the boards exist leaves gaps. This article explains how to build a test strategy across EVT, DVT, PVT, and production, and how to choose the right inspection and test methods for each.
Why Test Strategy Must Be Set Early
Testing has a multiplier effect. A defect caught at prototype validation costs an edit. The same defect caught at first article costs a rework. Caught in the field, it costs a recall. A test strategy set during NPI puts the right method at the right point, so defects are caught where they are cheapest. It also drives two things with long lead times: test fixtures and test programs. Both must be planned during NPI, not after the boards exist. Test programs and trained operators take time too, and both are scheduled during NPI rather than discovered at production start.
What a Test Strategy Decides
A complete test strategy answers four questions:
- What defects can this product have, and which methods catch them?
- What is covered at each stage — EVT, DVT, PVT, and production?
- What fixtures and programs are needed, and when must they be ready?
- What happens to a board that fails — rework, repair, or scrap?
The answers become the coverage plan, the fixture list, and the disposition rules. Without them, testing is improvised and coverage has holes. A strategy also decides what is not tested. No program tests everything; the question is which coverage is worth its cost. Documenting what is intentionally not covered — and why — prevents arguments later, and lets the customer make the trade-off with full information.
Testing in EVT: Proving the Design
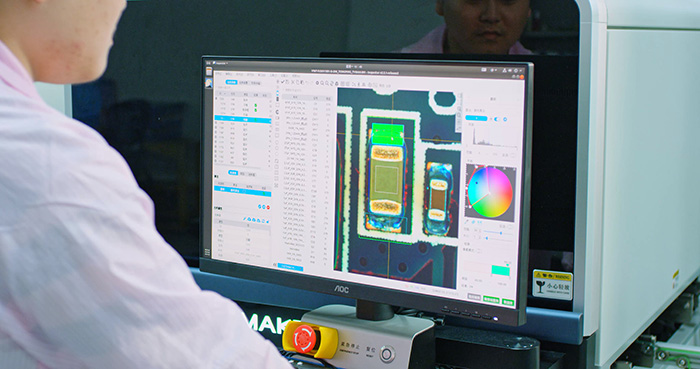
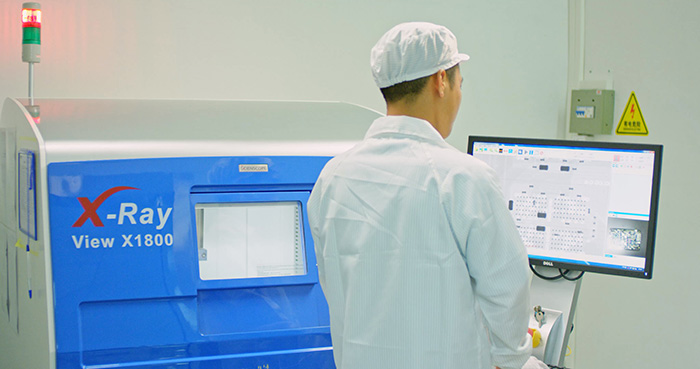
In engineering validation (EVT), the goal is to prove the design works at all. Quantities are small, the design is still changing, and the emphasis is on finding unknowns. Fixtureless methods fit this stage: AOI after reflow for visible joints, X-ray for hidden ones, and flying probe for electrical verification without a bed-of-nails fixture.
What to decide in EVT: the failure modes that matter for this design, and the baseline coverage the product will need. EVT is where the test strategy starts, not where it is finished. A useful EVT test record captures which defects appeared and where, because that list becomes the input to the coverage plan for DVT.
Testing in DVT: Coverage and Fixtures
In design validation (DVT), the design is stabilizing and the focus moves to coverage: does the test plan catch the defects that matter? This is the stage to finalize which nets need ICT or flying probe coverage, which joints need X-ray, and what the functional test must prove.
What to decide in DVT: the final test coverage plan and the fixture list. Test fixtures and programs are ordered here so they are ready for PVT. DVT is the last cheap place to change the strategy.
Testing in PVT: Proving the Process
In production validation (PVT), the design is frozen and the question is whether the process holds at volume. PVT uses the production test setup: the same AOI programs, X-ray, ICT or functional test, and fixtures that production will use. Yield is measured, failures are dispositioned, and the coverage plan is proven on real volume.
What to decide in PVT: the yield baseline and the disposition rules. If the test strategy has gaps, PVT is where they show up — while there is still time to fix them.
Testing in Production: Repeating the Plan
In production, the test strategy becomes a repeatable routine: the same inspection on every board, the same electrical and functional tests, the same records per batch. The strategy set during NPI is now executed without variation. Changes to test are treated like changes to design — controlled, reviewed, and documented. Records from production testing feed back into the next NPI: a failure mode seen at volume becomes a check in the next product's coverage plan.
Choosing Methods: AOI, X-ray, ICT, Flying Probe, FCT
- AOI catches visible placement and solder defects on every board, at low cost per board; it is the default first inspection after reflow.
- X-ray catches hidden joints — BGA, QFN, and bottom-terminated parts — where the joint is not visible to any camera.
- ICT gives fast, repeatable electrical testing at volume, at the cost of a bed-of-nails fixture with its own build lead time.
- Flying probe covers the same electrical faults without a fixture, suited to prototypes and low volume where setup must stay small.
- FCT (functional circuit test) proves the board operates as designed under power, confirming behavior that structural tests cannot.
No single method covers everything. The strategy combines them so that process defects, electrical faults, and functional behavior are each caught at the right stage.
A Worked Example: A Simple Coverage Plan
Take a medium-volume board with mixed SMT and a BGA at the center. A coverage plan built during NPI might look like this:
- AOI after reflow on every board, catching visible placement and solder defects.
- X-ray on the BGA and any fine-pitch bottom-terminated parts, catching hidden voids, bridges, and opens.
- ICT on the critical nets and power rails, catching opens and shorts that optical inspection cannot see.
- FCT on every board, loading firmware and verifying that the interfaces respond.
- Flying probe on the first boards of each build as a validation check before the ICT fixture is trusted.
The plan matches a method to each defect class and places each method where it is cheapest. It is written during NPI so the ICT fixture and the FCT jig are ordered before the boards exist. The same method choices apply to simpler boards, with fewer stages; the principle is that each defect class is covered at the cheapest point.

Fixtures and Their Lead Time
The practical limit on a test strategy is tooling. A bed-of-nails ICT fixture has a build time of its own, a functional test jig is product-specific, and both must exist before the boards are tested at volume. During NPI, the fixture list and its delivery dates become part of the schedule. Ordering the fixture before the design freezes risks paying for a change; ordering it after risks waiting. The resolution is to freeze the test points and the interface requirements as part of the design, so the fixture can be built in parallel with the rest of the program.
Test Data and the Yield Review
A test strategy is not finished when it is written; it is validated by data. During NPI, review the failure data at each stage: what fails, how often, and at which test. A failure Pareto shows where the real defects are, and coverage can be adjusted to catch them. A board that keeps failing functional test may need a better test program, or it may be revealing a design issue. The disposition rules — rework, repair, or scrap — are applied consistently from this data. Test data is the feedback loop that makes the NPI test strategy accurate instead of assumed.
Building the Test Coverage Plan
Build the coverage plan by working backward: start with what the product must not ship with, then choose the method that catches each class at the cheapest point. Document the plan in the NPI kickoff, agree it with the CM, and revisit it when the design or the failure data changes. A coverage plan written during NPI is a spec; one written later is a hope. The plan should be revalidated whenever the failure data changes the risk picture, not held as a fixed document. The plan is owned jointly — the customer decides what must not ship, and the CM proposes how to prove it.

FAQ
Q: What is a test strategy in PCBA NPI?
A: The plan for what to inspect and test at each stage — EVT, DVT, PVT, and production — including methods, fixtures, and disposition rules.
Q: Why is the test strategy set early in NPI?
A: Fixtures and test programs have long lead times, and defects are cheapest to catch at the earliest stage.
Q: Which test methods suit a prototype?
A: Fixtureless methods — AOI, X-ray, and flying probe — fit small, changing prototype quantities without tooling.
Q: What is the difference between testing in PVT and production?
A: PVT proves the process and coverage on real volume with production tooling; production repeats the proven plan without variation.
Shenzhen 1943 Technology Co., Ltd. defines the test strategy with each customer during PCBA NPI and carries it from prototype validation through production test.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08