What to Prepare Before Starting PCBA NPI: A Handoff Checklist
PCBA New Product Introduction (NPI) starts before the first board is built. What you prepare before the handoff decides how fast the program moves and how many surprises it contains. This article lists what a contract manufacturer needs from you — and what you should have decided yourself — before NPI begins.
Why Preparation Decides NPI Speed
The design is the fastest thing in an NPI program; everything else follows it. If the file package is complete, the BOM is sourcing-ready, and the test plan is agreed, the program can start the day the files arrive. If any of those is missing, the program stops while the missing piece is assembled. Preparation does not add time to NPI; it removes the stops. The preparation that takes an afternoon at the start of NPI is the preparation that would otherwise take weeks in the middle of it.
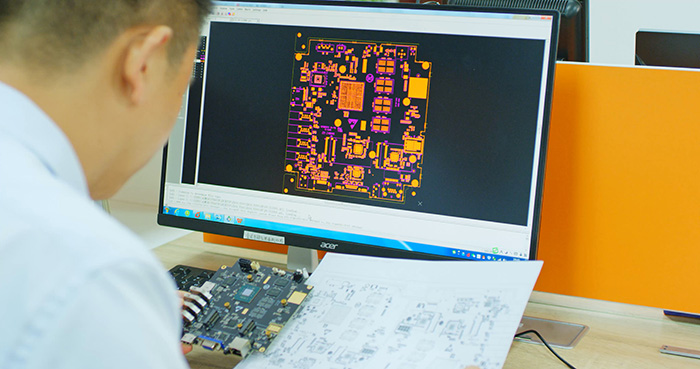
1. The Controlled File Package
The first thing a CM needs is a complete, revision-matched package:
- Gerber or ODB++ files, the latest revision.
- Drill files consistent with the board outline.
- BOM with manufacturer part numbers and quantities per board.
- Centroid (pick-and-place) file matching the BOM reference designators.
- Assembly drawing and fabrication notes.
- Fabrication and assembly specifications, where required.
The fabrication specification — material, thickness, finish, and impedance requirements — is part of the package too, because it decides what the bare board costs and how it is made. A package that includes it removes questions at the fabrication stage.
The rule: one revision for everything. Mixed revisions are the single most common cause of a wrong first build. Confirm the package before sending, and expect the CM to verify it at the design handoff.
2. A Sourcing-Ready BOM
The BOM is not just a parts list; it is the procurement plan. A sourcing-ready BOM has, for each line: manufacturer part number, description, quantity, package, reference designators, lifecycle status, and approved alternates with substitution rules.
Why it matters: component sourcing is usually the longest stage of NPI. A BOM without part numbers forces assumptions and produces unreliable quotes. A BOM with alternates gives the buyer a second path when the first choice is unavailable. Review the BOM for availability and risk before the handoff, not after.
3. Test Requirements and Coverage
Testing is cheaper to plan than to improvise. Before NPI starts, decide:
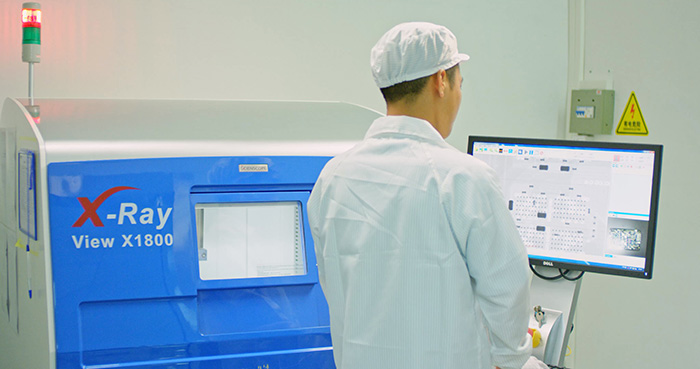
- Which test strategy applies: AOI, X-ray, ICT, flying probe, functional test.
- What must be covered for this product — hidden joints, critical nets, firmware behavior.
- Who writes the functional test program, and what fixtures are needed.
Why it matters: fixtures and programs have their own lead time. Deciding the test strategy during NPI means the fixture is ready when the boards are. Deciding it later means validation waits on tooling. Coverage agreed in writing — what is inspected, what is tested, and what fixture is ordered — prevents the fixture arriving after the boards do.
4. The DFM-Readiness Review
Before the files are sent, run your own check against the basics: pad sizes, clearances, test points, fiducials, and panelization. The CM will run its own DFM review, but your pre-check catches the obvious issues and makes the CM's review more useful.
Why it matters: a DFM review at the start of NPI returns findings at the cheapest possible time. Issues found before tooling are edits; issues found after are re-spins. A useful DFM review at this stage checks at least pads, clearances, test points, fiducials, and panelization, and returns findings in terms of what to change and why.
5. Tooling and Fixture Decisions
Decide what tooling the program needs and who pays for it:
- Production stencils, if volume justifies them over a prototype stencil.
- Test fixtures for ICT or functional test.
- Panel design and any assembly jigs.
Why it matters: tooling is one-time cost with its own lead time. Ordering it when the design is stable — not before, not after — keeps the program on schedule without paying twice.
6. Communication and the Named Contact
An NPI program runs on decisions. Before it starts, agree who the engineering contact is on each side, what the review points are, and how changes are approved.
Why it matters: the DFM report raises questions, sourcing raises alternates, and test raises coverage gaps. If the answers require a meeting to arrange, the program stalls. A named contact with a defined escalation path keeps decisions moving.
7. The NPI Kickoff Document
A short kickoff document ties the program together. It should state:
- The product and revision under NPI.
- The test strategy and product class.
- The sourcing model — customer-supplied or CM-procured.
- The schedule, including long-lead part dates.
- The approval points for changes.
Why it matters: the kickoff document is the single source of truth. When assumptions change — and they will — the document is the baseline everyone returns to.
Common Handoff Gaps and How to Close Them
The most common gaps at the PCBA NPI handoff, and the fix for each:
- Mixed file revisions: close it by checking every file against the same revision before sending.
- BOM without manufacturer part numbers: close it by filling in MPNs, quantities, and reference designators before the handoff.
- No alternates for risky parts: close it by approving alternates at BOM freeze, not during sourcing.
- Undefined test plan: close it by writing the test strategy in the kickoff document, including coverage and fixtures.
- No single contact: close it by naming one engineering contact per side and one escalation path.
Most handoff problems are not technical; they are missing decisions. Closing the gaps before the files arrive is faster than discovering them after the schedule has started.
What Happens After the Handoff
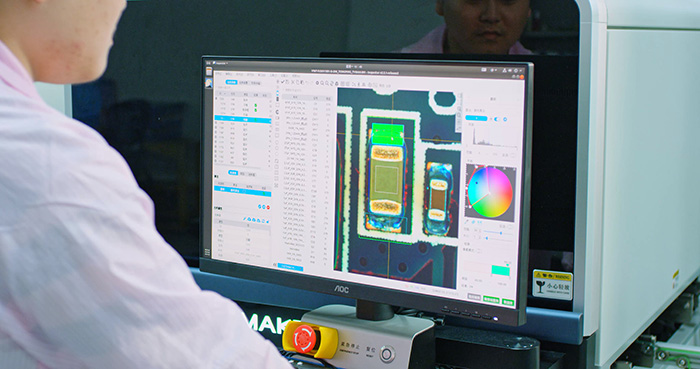
Once the package arrives, a good CM responds in a predictable order: verify the files, run the DFM review, check BOM availability, return findings and a quote, and then hold the kickoff against the document. The speed and quality of this response is the first real signal of how the program will run. A CM that returns actionable DFM findings and a sourcing risk list early is managing your risk; one that returns a quote only is not. The handoff is not the end of your preparation — it is the start of a review loop that ends at the approved sample.
Signs the Handoff Is Ready
You know the handoff is ready when you can answer yes to five questions: is the file package complete and one revision; is the BOM sourcing-ready with alternates; is the test strategy decided; is the DFM pre-check done; and is one contact named on each side. If any answer is no, the missing item is exactly what will stop the program. Completing these five before the files are sent is the difference between an NPI that starts on time and one that starts late.
What the CM Owes You Back
The handoff is a two-way exchange. In return for a complete package, the CM owes you specific outputs: a DFM report with actionable findings, a sourcing risk list, a test coverage proposal, and a schedule with the long-lead dates. If any of these is missing from the response, the program is missing part of its plan. Reviewing what the CM returns against the kickoff document keeps the handoff honest, and it is the fastest way to tell whether the program will run on agreed assumptions or on assumptions that were never stated.

The Handoff Checklist at a Glance
|
Item |
Status before NPI starts |
|
File package |
Complete, one revision, verified |
|
BOM |
Sourcing-ready, alternates approved |
|
Test strategy |
Decided, fixtures ordered |
|
DFM pre-check |
Run, findings reviewed |
|
Tooling |
Planned, timed to design stability |
|
Communication |
Named contact, approval path |
|
Kickoff document |
Written, agreed, revision-controlled |
FAQ
Q: What does a CM need before PCBA NPI starts?
A: A complete, revision-matched file package; a sourcing-ready BOM; a decided test strategy; and an agreed point of contact.
Q: Why is the BOM reviewed before NPI begins?
A: Component sourcing is usually the longest stage, so availability and alternates must be settled before the schedule depends on them.
Q: What is an NPI kickoff document?
A: A short document stating the product, test strategy, sourcing model, schedule, and approval points — the single source of truth for the program.
Q: When should test fixtures be ordered in NPI?
A: As soon as the test strategy is decided and the design is stable, so the fixture is ready when the boards are.
Shenzhen 1943 Technology Co., Ltd. works with customers at the PCBA NPI handoff — verifying the file package, reviewing the BOM, and agreeing the test strategy before the first board is built.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08