When Is a PCBA Ready to Move From NPI to Production?
Transitioning a Printed Circuit Board Assembly (PCBA) from New Product Introduction (NPI) to full-scale volume production is a pivotal phase in hardware development. Transitioning too early risks high defect rates, line stoppages, and expensive field recalls. Delaying the transition, however, causes missed market windows and inflated engineering overhead.
Determining when an NPI project is ready to ramp up requires rigorous engineering verification, repeatable manufacturing processes, and a stable supply chain. At Shenzhen 1943 Technology Co., Ltd., our one-stop NPI engineering team uses a data-driven validation framework to evaluate mass-production readiness.
Technical Prerequisites for Mass Production Readiness
A PCBA design transitions out of the NPI pilot stage only when it satisfies performance, process yield, and quality control criteria across four core engineering domains.
1. Design & DFM Sign-Off
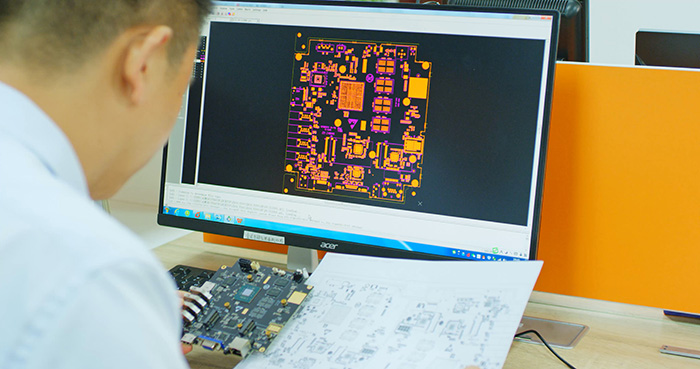
A prototype may function correctly on a lab bench, but mass production requires layout optimizations for automated Surface Mount Technology (SMT) and Through-Hole Technology (DIP/THT) lines.
- Design for Manufacturability (DFM): Pad geometry, trace clearances, thermal relief connections, and copper balance must be verified to prevent defects such as component tombstoning, solder bridging, and board warp during reflow.
- Design for Assembly (DFA): Clear fiducial placement, component pitch adjustments, and consistent orientation for automated pick-and-place machines must be finalized.
- Panelization Design: PCB panel layouts must include adequate breakup tabs, v-scoring tolerances, and tooling holes to withstand automated routing or de-paneling without stress cracking nearby ceramic capacitors.
2. Component Procurement & BOM Validation
Supply chain volatility can halt a production line just as quickly as a technical defect.
- Bill of Materials (BOM) Scrubbing: All components must be active, with lifecycle statuses verified (avoiding End-of-Life or Not Recommended for New Designs status).
- Approved Vendor List (AVL) Multi-Sourcing: Alternate components for passive parts, connectors, and key pin-to-pin compatible integrated circuits (ICs) must be qualified to mitigate component shortages.
- Moisture Sensitivity Level (MSL) & Storage Controls: High-MSL components require verified baking and vacuum-sealing protocols prior to SMT placement.
3. Process Stability and First Pass Yield (FPY)
During pilot runs—typically Design Verification Test (DVT) and Production Verification Test (PVT)—the assembly line is monitored to establish process control metrics.
- First Pass Yield Thresholds: FPY measures the percentage of assemblies that pass all inspection gates without rework. Transitioning to volume production generally requires an FPY of 95% to 98% or higher, depending on board complexity.
- Reflow Profile Optimization: SMT reflow temperature profiles must be tuned to match board density, thermal mass, and specific lead-free solder paste formulations.
- CPK and Process Capability: Critical process steps must demonstrate statistical repeatability (Cpk ≥1.33\ge 1.33≥1.33$\ge 1.33$).
4. Comprehensive Testing Strategy Implementation
Mass production lines rely on fast, deterministic test coverage to capture defects early in the flow.
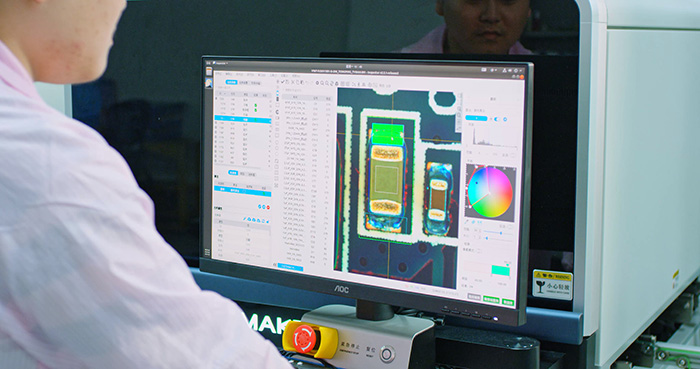
- Automated Optical Inspection (AOI): Verified programming for solder joint fillets, component presence, polarity, and alignment.
- X-ray Inspection (AXI): Required for complex packages such as Ball Grid Arrays (BGAs) and Quad-Flat No-Leads (QFNs) to inspect internal voiding ratios and solder bridging beneath hidden leads.
- In-Circuit Testing (ICT) or Flying Probe: Validates nets for shorts, opens, and passive component values.
- Functional Circuit Testing (FCT): Dedicated test fixtures and automated firmware flashing routines must be deployed to validate complete operational logic under load.
NPI Gate Comparison: EVT vs. DVT vs. PVT
|
Stage |
Primary Objective |
Typical Lot Size |
Exit Criteria for Next Phase |
|---|---|---|---|
|
Engineering Validation Test (EVT) |
Prove core functional operation and schematic logic. |
5 – 20 units |
Core hardware functions operate; initial DFM report generated. |
|
Design Verification Test (DVT) |
Validate form factor, mechanical fit, and environmental reliability. |
50 – 200 units |
Board layout finalized; no major hardware revs needed; thermal & stress tests passed. |
|
Production Verification Test (PVT) |
Validate assembly line tools, speed, yield, and test fixtures. |
100 – 1,000+ units |
FPY meets target; assembly instructions locked; test cycle time optimized. |
|
Mass Production (MP) |
High-volume continuous manufacturing. |
Scalable |
Stable yield, active quality monitoring, optimized unit costs. |
Key Performance Metrics Checklist
Before signing off on the NPI-to-Production release, confirm that the following engineering metrics have been satisfied:
-
[ ] Engineering Change Orders (ECOs) Locked: Zero pending hardware design revisions or component swaps.
-
[ ] Assembly Process Documents Complete: Standard Operating Procedures (SOPs) fully drafted and approved for each workstation.
-
[ ] Tooling and Fixtures Qualified: SMT stencils, selective soldering pallets, routing jigs, and FCT test beds are validated and backed up.
-
[ ] Traceability Framework Active: Barcode or matrix code scanning system configured to track lot numbers, reel batches, and inspection results down to individual PCBA serial numbers.

Frequently Asked Questions (FAQ)
Q1: What is the main difference between DVT and PVT in PCBA manufacturing?
DVT (Design Verification Test) focuses on verifying that the hardware design meets all physical, electrical, and environmental performance specifications. PVT (Production Verification Test) uses the final production-equivalent design to evaluate the stability, speed, and yield of the manufacturing process itself using actual volume tooling and assembly lines.
Q2: How does a low First Pass Yield (FPY) during the NPI stage impact mass production?
A low FPY indicates underlying design flaws, unstable solder profiles, or component placement issues. Attempting volume production with a low FPY leads to excessive manual rework, latent solder joint defects, elevated scrap rates, and unpredictable delivery schedules. Issues must be resolved during PVT before ramping volume.
Q3: Why is DFM review critical during early NPI prototyping?
Design for Manufacturability (DFM) reviews identify layout issues—such as incorrect land patterns, unbalanced thermal traces, or insufficient clearance around BGA packages—before bare boards are fabricated. Catching these items early prevents costly PCB respins and shortens overall development cycles.
Q4: How do automated test fixtures (FCT) shorten the transition from NPI to volume assembly?
Manual testing during early prototyping is slow and prone to human error. Developing automated Functional Testing (FCT) fixtures and programmed firmware loaders during the NPI phase allows unit test times to drop from minutes to seconds, establishing the high-throughput testing gate required for scalable mass production.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08