PCBA Pilot Production Platform: NPI Line Planning Guide
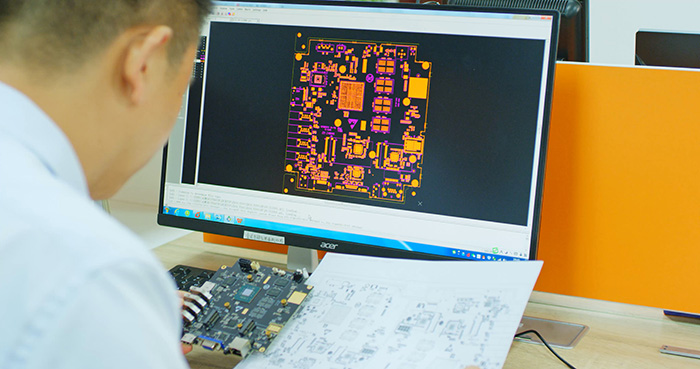
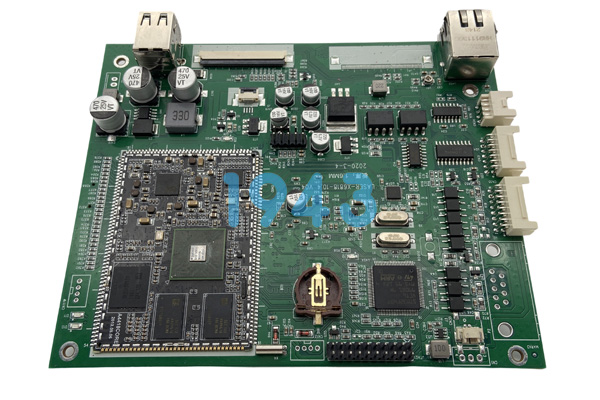
A pilot production platform is the physical infrastructure that makes NPI possible. It is neither a research laboratory nor a mass production line, but an engineered validation environment between the two. A well-designed pilot platform enables small-batch manufacturing under production-representative conditions, generating the data required to prove process capability and establish production standards.
1943 Technology operates a dedicated PCBA NPI pilot line designed specifically for this purpose.
The Strategic Role of the Pilot Platform
The pilot platform serves two functions: validation and translation.
Validation confirms that design outputs are manufacturable, processes are stable, materials are suitable, and the product performs reliably under system-level integration. Translation converts validated knowledge into standard manufacturing documentation.
Compared to production lines, pilot platforms offer higher flexibility for rapid product changeover, higher measurement density with comprehensive instrumentation, and cross-functional engineering staff rather than single-skill operators.
Pilot Line Layout
A typical PCBA pilot line follows a U-shaped or linear flow:
- Incoming Inspection: Receives PCBs, components, and consumables, verifying material quality before assembly commitment.
- SMT Assembly: Solder paste printing, component placement, reflow soldering, with inline SPI and AOI.
- Through-Hole Processing: Manual or automated insertion, wave or selective soldering.
- Test and Verification: ICT, FCT, and environmental stress screening.
- Final Assembly and Packaging: Mechanical integration and shipment preparation.
- Rework and Analysis: Positioned adjacent to the line for immediate failure analysis without flow disruption.
Each zone is sized for accessibility and instrumentation, not maximum throughput.
Equipment Selection Criteria
Pilot line equipment prioritizes capability over speed:
- Compatibility: Coverage of mainstream requirements including fine-pitch QFP, BGA, CSP, and bottom-terminated components.
- Precision: Exceeds typical production specifications, enabling detection of process boundary conditions.
- Data Connectivity: Digital interfaces for exporting temperature profiles, placement coordinates, and inspection results.
- Adjustability: Rapid parameter modification without extended calibration cycles.
Implementation Path
Phase 1: Requirements Analysis Defines validation scope: product critical characteristics, primary focus areas, and acceptance criteria per domain.
Phase 2: Preparation Material preparation confirms BOM completeness. Documentation gathers design files and test programs. Equipment verifies calibration. Personnel are assigned and trained.
Phase 3: Execution and Monitoring Engineers maintain continuous presence. First-article inspection prevents error propagation. Real-time parameter monitoring captures drift. Defect logging records every anomaly. Escalation protocols trigger immediate technical review for major issues.
Phase 4: Data Analysis and Improvement Between runs, data undergoes comprehensive analysis. Yield rates, defect Pareto rankings, and parameter statistics drive improvement actions scheduled for subsequent run verification.
Phase 5: Standardization and Knowledge Transfer Generates complete documentation: process verification reports, production standards, inspection criteria, work instructions, and closed-loop issue registers.
Data Management
Modern pilot platforms require digital data management. MES integration enables automatic parameter capture, real-time defect entry, and automated reporting. Visualization tools generate yield trends, defect Paretos, and capability distributions. Historical databases accumulate across projects, enabling pattern recognition.
1943 Technology has invested significantly in this infrastructure. Our pilot platform captures data automatically from reflow ovens, SPI systems, placement equipment, and test stations, feeding structured analysis workflows.

Bridging Pilot and Production
The ultimate measure of a pilot platform is production transition effectiveness. 1943 Technology ensures this through:
- Process Consistency: Validated parameters are directly transferable to client production lines.
- Operator Training: Production operators train on the pilot platform before mass production launch.
- Rapid Response: Production issues are reproduced and analyzed on the pilot platform without disrupting manufacturing schedules.
Frequently Asked Questions
How does a pilot platform differ from a prototype build line? Prototype lines focus on functional validation using best-case materials and manual techniques without concern for repeatability. Pilot platforms simulate production environments, validating capability, consistency, and efficiency while generating transferable standards.
What inspection equipment is essential? Minimum essentials include SPI, AOI, X-ray, ICT, and FCT. Depending on requirements, additional instruments such as thermal imaging systems may be necessary.
What capabilities should pilot line engineers possess? Multidisciplinary competencies: PCB design and DFM, SMT and through-hole processes, test methodology, statistical analysis, and structured problem-solving. Communication skills are equally important for coordinating across stakeholders.
Should pilot platforms handle production volumes? No. They are optimized for validation efficiency, not throughput. Diverting pilot capacity to production degrades validation effectiveness and extends NPI timelines.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08