PCBA Process Verification: SMT, DIP, Assembly Feasibility
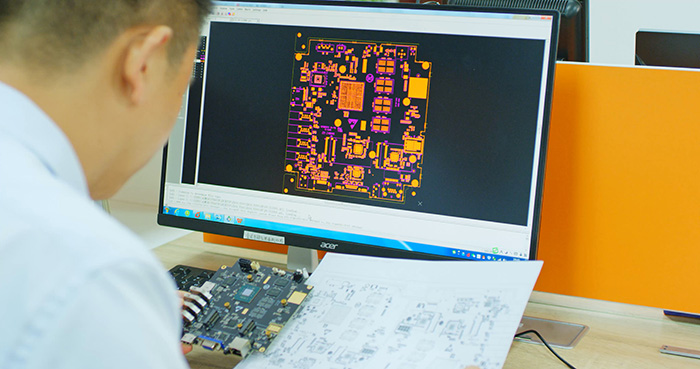
Process verification is the technical core of PCBA NPI. While design verification confirms that a board can theoretically be built, process verification confirms that it can actually be built—repeatedly, with controlled variation, and within specification. This phase subjects the product to the full manufacturing chain, collecting data at every step to prove capability before mass production.
At 1943 Technology, process verification is a data-driven engineering exercise, not empirical trial-and-error.
Solder Paste Printing
Solder paste printing quality directly influences reflow outcomes. Verification addresses stencil design, printing parameters, and print quality detection.
Stencil design verification confirms aperture dimensions, thickness, and geometry match pad requirements. For 0.4 mm pitch QFN devices, apertures typically require 10–15% area reduction to prevent solder balling.
Printing parameter verification optimizes print speed, squeegee pressure, and separation speed through structured experimentation. Different solder paste chemistries and PCB surface finishes require different parameter sets.
Print quality verification uses SPI to measure paste volume, height, and area on every board. Cpk ≥ 1.33 confirms statistical capability.
Component Placement
Placement verification focuses on accuracy and force control.
Placement accuracy is measured for each component category. Small passives (0201, 0402) and bottom-terminated devices (BGA, QFN) receive particular attention. X/Y offset and rotational deviation are measured against specification limits.
Placement force is verified to prevent component cracking. Ceramic capacitors and crystals are especially sensitive to excessive pressure. Force profiles are validated against manufacturer specifications.
Feeder stability is confirmed across the run. Tape and vibratory feeders are checked for consistent component presentation, eliminating mis-picks and flipped components.
Reflow Soldering
Reflow soldering introduces the highest thermal stress and greatest defect risk.
Reflow profile verification develops a temperature curve specific to the product. The profile must accommodate solder paste specifications (typically 235–245°C peak for lead-free alloys), PCB thermal mass, and component thermal sensitivity. Critical parameters include ramp rate, soak time, time above liquidus, and cooling rate.
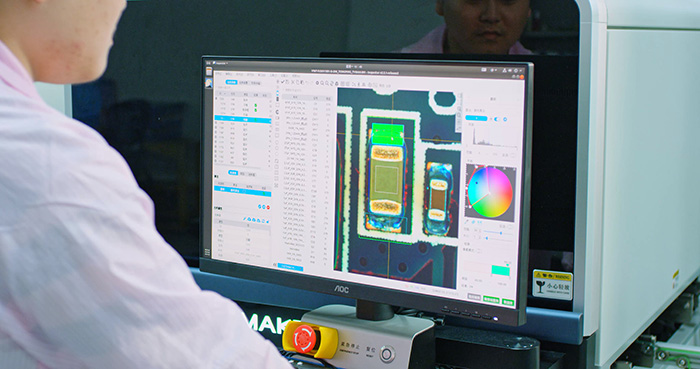
Post-reflow inspection combines AOI for visible defects (bridging, tombstoning, insufficient solder) and X-ray for hidden joints (BGA voiding, head-in-pillow). BGA void rates are quantified against IPC-A-610 criteria.
DIP and Wave Soldering
For through-hole components, insertion and wave soldering require separate verification.
Insertion verification checks lead forming, polarity orientation, and insertion height. Polarized devices must have clear orientation indicators and effective polarization protection.
Wave soldering verification optimizes flux density, preheat temperature, wave height, and contact time. Through-hole fill percentage is the primary quality metric, with IPC Class 2 requiring 75% minimum fill. Solder pot chemistry is monitored for copper and iron contamination.
Hand soldering verification is performed for components unsuitable for wave soldering. Accessibility, iron temperature control, and joint consistency across operators are evaluated.
Testing Process Validation
Testing is the final barrier against defect escape.
ICT Verification confirms test point coverage, program stability, and probe contact reliability. Coverage targets typically exceed 80% of networks. False pass and false fail rates are measured across multiple units.
FCT Verification validates that functional test programs cover all specified features with appropriately set limits. Test fixture durability and contact reliability are assessed under repeated cycling.
Burn-in Verification confirms that stress conditions accelerate latent defect exposure without over-stressing normal product populations.

Data Analysis Methods
Process verification relies on statistical methods:
- SPC monitors critical parameters in real time, distinguishing common cause from special cause variation.
- Pareto Analysis categorizes defect frequencies, directing resources toward the vital few defect modes.
- DOE systematically varies parameters to identify main effects and interactions, achieving optimal settings efficiently.
1943 Technology integrates these methods into every engagement. Our NPI lines feed automated data collection directly into analysis platforms, ensuring decisions are evidence-based.
Frequently Asked Questions
What is the difference between process development and verification? Process development creates the initial strategy. Process verification validates that the developed process performs as intended under real manufacturing conditions. Development is prescriptive; verification is confirmatory.
How many pilot runs are typically required? Two to four runs are typical. The first exposes major issues; the second validates corrective actions; the third confirms stability. Complex products may require additional iterations, each separated by thorough data analysis.
What defines successful process verification? Cpk ≥ 1.33 for critical parameters; yield rates meeting mass production targets; major defect modes resolved or controlled; validated work instructions; test coverage and detection rates meeting specification. All criteria must be satisfied simultaneously.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08