Through-Hole + SMT Mixed Technology NPI Best Practices
Why Mixed Technology Still Matters in Modern PCBA
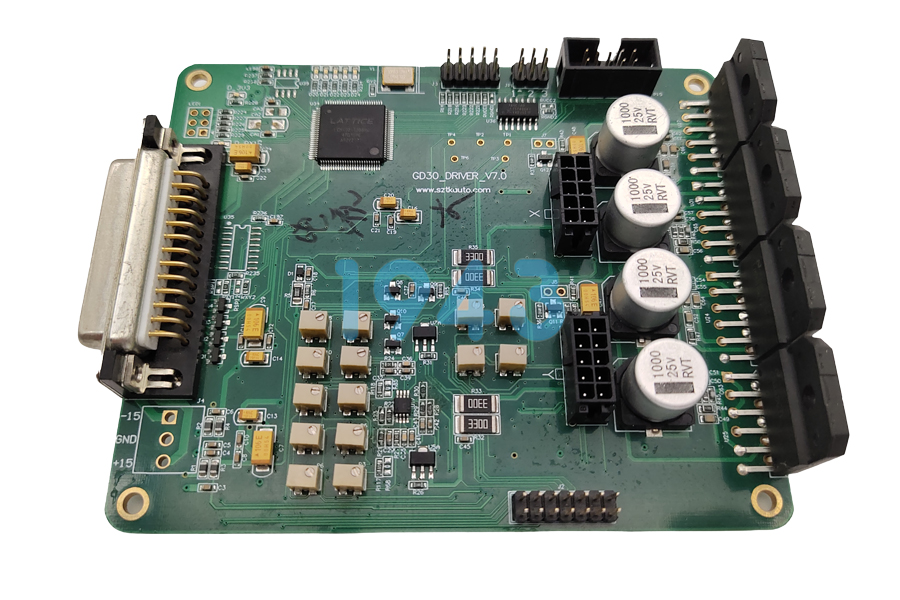
Even as surface mount technology dominates most board designs, a significant share of electronic products still combine SMT components with through-hole devices (THD). Connectors, electrolytic capacitors, transformers, power inductors, large mechanical relays, and certain high-current or high-voltage components continue to require through-hole mounting for mechanical strength, thermal endurance, and current-carrying capability.
This combination—what the industry calls mixed technology assembly—creates one of the most challenging scenarios in PCBA manufacturing. During New Product Introduction (NPI), engineering decisions made in the first few builds directly determine yield, reliability, and time-to-market. A well-executed mixed technology NPI process reduces rework cost and shortens the gap between prototype and mass production.
At 1943 Technology, mixed technology projects account for a notable portion of the PCBA New Product Introduction Services we deliver to industrial control, medical instrumentation, energy storage, and telecommunications customers.
1. Understanding the Three Common Mixed Technology Scenarios
Before establishing any process, it helps to identify which mixed technology configuration applies.
Scenario A — Single-side SMT + single-side THT SMT components are placed on the top side, through-hole leads are inserted from the bottom, and the board passes through a wave soldering step for the THD side. This is the simplest and most common layout.
Scenario B — Double-side SMT + through-hole Both sides carry SMT components, while selected through-hole parts are still required. Pin-in-paste (PiP) reflow or selective soldering becomes necessary to avoid damaging SMT components on the bottom side during wave soldering.
Scenario C — Mixed on the same side Both SMT and through-hole components share the same PCB side, often clustered near connectors or power sections. This layout requires careful solder joint inspection and stencil design adjustments.
Recognizing which scenario applies early in the NPI phase prevents rework loops later.
2. DFM Review: The Most Cost-Effective Step in Mixed Technology NPI
Roughly 70% of mixed technology defects originate from design choices that were never questioned. A structured DFM (Design for Manufacturing) review before the first prototype run dramatically reduces iterations.
Key items to verify:
- Hole-to-pad clearance — ensure through-hole pads are not buried under SMT land patterns with no visible solder joint.
- Component spacing — keep at least 2.5 mm between through-hole components and nearby SMT parts to avoid shadowing and solder bridges during wave soldering.
- Component orientation — mark polarity, pin 1, and orientation identically in Gerber, BOM, and assembly drawings.
- Via tenting — open vias near wave soldering pads can wick solder away from THT joints and cause insufficient fillets.
- Thermal relief on THT pads — for boards with internal copper planes, four-spoke thermal relief patterns improve hole fill during wave soldering.
- Keep-out zones — define clearance around connectors and tall components to allow fixture contact and selective soldering nozzles.
A reliable NPI partner reviews these items in ECAD-native software before tooling is cut, which is considerably cheaper than re-spinning a stencil or a pallet.
3. Soldering Process Selection: Wave, Selective, or Pin-in-Paste
Three soldering methods dominate mixed technology assembly. Choosing the wrong one is a frequent source of NPI delays.
3.1 Wave Soldering with Fixturing
Wave soldering remains the most economical method for single-side THT production. Pallets (solder masks) protect SMT components on the top side when the board passes over the wave.
When to use: high-volume THT, simple single-side mixed boards, components tolerant of contact soldering temperature.
Watch points:
- Pallet material must withstand repeated thermal cycling.
- Pallets add 10–20 seconds to cycle time per board.
- Selective fluxing may be required for mixed thermal mass boards.
3.2 Selective Soldering
Selective soldering uses a programmable mini-wave that contacts only specified THT leads. No pallet is required, and no SMT component is exposed to the wave.
When to use: double-sided SMT boards with THD, low-to-medium volume, prototypes and pilot runs, products with tight thermal budgets.
Watch points:
- Flux must be applied precisely to avoid residue on SMT areas.
- Programming the soldering profile per THT lead adds NPI time but pays back in higher yield.
- Nitrogen inert environment is often used in selective soldering, though it is not the only option—carefully tuned flux activation and dwell time can deliver reliable joints in air atmosphere as well.
3.3 Pin-in-Paste Reflow
PiP deposits solder paste into the through-hole using a specially designed stencil, then reflows the board just like an SMT process. It eliminates wave soldering entirely for those joints.
When to use: board real estate is tight, no wave or selective line is available, components have flat enough leads to allow paste filling, plating thickness supports reliable hole fill.
Watch points:
- Hole-to-pad ratio and stencil aperture design are critical.
- Paste volume must be calculated, not guessed.
- Some through-hole components (large transformers, heavy connectors) may require additional preheating.
1943 Technology routinely applies all three methods during NPI builds, choosing based on the specific board geometry, volume, and existing equipment set rather than a one-size-fits-all approach.
4. Process Sequencing Strategy
Process sequencing determines how many times a board is heated and how many times it is handled. More heat cycles mean higher risk of pad lifting, delamination, and solder joint fatigue.
A typical mixed technology sequence:
- SMT paste print (top side)
- SMT placement (top side)
- Reflow (top side)
- SMT paste print (bottom side) — for double-side SMT
- SMT placement (bottom side)
- Reflow (bottom side)
- Through-hole insertion — manual, semi-automatic, or pin-in-paste during SMT step
- Selective or wave soldering for THD
- Cleaning (if required)
- AOI / X-ray / flying probe inspection
When possible, perform through-hole soldering after both SMT reflow steps. This avoids exposing SMT components to a second reflow cycle.
5. Stencil Design for Mixed Technology
The stencil is often overlooked, yet it directly controls paste volume on both SMT pads and PiP apertures.
- Aperture reduction — standard SMT apertures are usually reduced by 10–20% to prevent solder balls; PiP apertures follow the inverse logic, often requiring 100–110% of pad size to ensure hole fill.
- Step-up or step-down stencils — useful when THT pads sit at a different height than surrounding SMT components.
- Two-print approach — for boards with both fine-pitch SMT and PiP, a second print with a different stencil or foil insert can improve consistency.
6. Inspection Strategy for Mixed Technology Boards
Each soldering method requires different inspection priorities.
| Process | Primary Inspection | Secondary Check |
|---|---|---|
| SMT Reflow | SPI, AOI, X-ray for BGA/QFN | Visual, ICT |
| Wave Soldering | AOI for bridges/insufficient solder | X-ray for hidden joints |
| Selective Soldering | AOI + selective profile log | Visual + pull test |
| Pin-in-Paste | X-ray for hole fill percentage | Cross-section on first article |
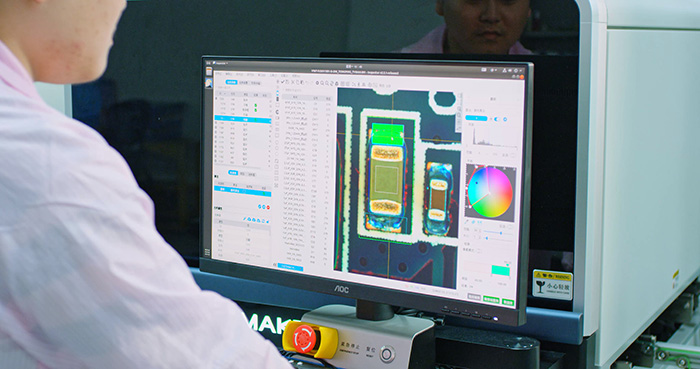
First-article inspection on mixed technology boards should always include cross-sectioning of representative THT joints to validate hole fill, wetting angle, and intermetallic formation.
7. Common Defects and Root Causes
Insufficient hole fill (THT) Root cause: insufficient preheat, low thermal relief, fast conveyor speed, wave contact height too low. Adjust preheat ramp and contact dwell.
Solder bridges between SMT pads after wave soldering Root cause: missing or damaged pallet area, flux contamination outside intended zones, stencil misregistration on bottom side.
Pad lifting after selective soldering Root cause: excessive dwell time, single-side copper balance missing, repeated rework. Modify thermal profile and consider preheating.
Solder balls on SMT side after PiP reflow Root cause: paste volume too high in through-hole apertures, reflow ramp rate too fast, aperture aspect ratio mismatched.
White residue after cleaning Root cause: flux type incompatible with cleaning chemistry, insufficient rinse, board held too long before cleaning.
Documenting these defect modes in an NPI feedback loop helps both the design and process engineering teams improve future revisions.
8. NPI Workflow That Reduces Time-to-Production
A mature NPI process for mixed technology boards typically follows this rhythm:
- File intake and design review — Gerber, BOM, centroid, drawings, and any mechanical files. DFM and DFA (Design for Assembly) feedback provided within 24–48 hours.
- Process planning — soldering method selection, stencil design, fixture requirements.
- First article build — small lot (5–25 units) under controlled conditions.
- First article inspection — cross-section, AOI, ICT, functional test as applicable.
- Yield analysis and feedback — defect Pareto shared with the customer's engineering team.
- Process lock-down — SOPs, work instructions, fixture drawings, and inspection criteria finalized.
- Pilot run — 50–200 units to validate process repeatability.
- Mass production ramp-up — transferred to the appropriate production line with verified process capability.
1943 Technology structures its PCBA New Product Introduction Services around this workflow, providing a single engineering point of contact from DFM review through pilot build. The goal is to compress what is often a 6–10 week learning cycle into a 3–5 week decision-driven cycle.
9. Practical Tips from Real Mixed Technology Builds
- Always order 5–10% extra first-article units; expect rework on the very first lot.
- Pre-bake moisture-sensitive components (MSL 2 and higher) before SMT assembly, especially if THT soldering will subject them to a second thermal event.
- Keep a soldering iron and rework station ready during first article—some joints will need touch-up regardless of process maturity.
- Use the same solder alloy throughout (e.g., SAC305) for SMT and THT unless thermal budget absolutely requires otherwise.
- Reserve connectors and large mechanical parts for the final insertion step to avoid manual handling damage to already-reflowed SMT components.
- Photograph the first article from every relevant angle and attach to the build report. Future operators will thank you.

Conclusion
Mixed technology PCB assembly is not a relic of older electronics—it is a deliberate design choice that demands disciplined NPI engineering. The combination of SMT precision and through-hole mechanical strength creates boards that perform in demanding environments, but only when DFM, process sequencing, soldering method, and inspection strategy are aligned from day one.
Treating mixed technology NPI as an engineering discipline rather than a series of disconnected production steps is the single biggest predictor of whether a new product will reach mass production on schedule.
Frequently Asked Questions (FAQ)
Q1: When should I choose pin-in-paste instead of wave soldering for through-hole components? Pin-in-paste is preferred when the board is double-sided SMT with limited space for wave fixtures, when production volume does not justify a dedicated wave line, or when the through-hole components have flat leads and reasonable hole aspect ratios. For high-current or large thermal mass parts, wave or selective soldering typically produces more reliable joints.
Q2: How many times will my board be heated during mixed technology assembly? A typical double-side SMT plus through-hole board experiences two reflow cycles and one selective or wave soldering cycle—three thermal events in total. With careful process planning, the third event can sometimes be absorbed into the second reflow (PiP), reducing the total to two. Each additional thermal cycle increases the risk of pad lifting and component damage.
Q3: What is the most common defect in mixed technology NPI builds? Insufficient through-hole fill on the first wave or selective soldering run is the most frequently observed issue, particularly on boards with heavy internal copper planes. The fix is usually a combination of thermal relief adjustment, preheat optimization, and contact dwell time tuning, rather than a wholesale process change.
Q4: How does 1943 Technology support customers who do not yet have a finalized BOM? Early-stage customers can provide preliminary BOMs, reference designs, or even functional requirements. The engineering team at 1943 Technology performs component selection guidance, second-source suggestions, and DFM feedback during the pre-NPI phase, ensuring that the BOM is both manufacturable and cost-stable before tooling is committed.
Shenzhen 1943 Technology Co., Ltd. — One-stop PCBA New Product Introduction Services, from DFM review and prototype build to pilot run and mass production ramp-up.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08