Creating a Robust NPI Risk Management Plan for Electronics
In electronics manufacturing, a new product introduction (NPI) risk management plan is not a static checklist. It is a working document that follows a product through PCBA prototype assembly, pilot production, and ramp. The plan should capture risks that affect manufacturability, component availability, test coverage, firmware readiness, supply chain stability, and process repeatability.
Many NPI delays are not caused by a single failure. They result from risks that were identified but never assigned to an owner, or from issues discovered too late to correct without another board spin. A structured risk management plan closes that gap.
This article outlines a practical framework for creating an NPI risk management plan for electronics, with emphasis on PCBA manufacturing and test readiness.
Why NPI Risk Management Needs a Dedicated Plan
Electronics NPI differs from standard project risk management because the risks are highly interdependent. A component shortage can force a last-minute substitution, which changes solder joint reliability or signal integrity. A missing test point can allow a latent defect to pass into pilot production. A firmware version mismatch can make an otherwise functional PCBA fail final test.
A dedicated NPI risk plan treats design, assembly, test, and supply chain as one connected system. It documents risks by phase, assigns ownership, and sets review points before each build.
Risk Categories to Include in an Electronics NPI Plan
A practical risk register for PCBA new product introduction should include these categories:
1. Design Maturity Risk
- Unresolved schematic or layout changes
- Incomplete design reviews
- Missing simulation or signal integrity checks
- Unclear version control for design files
- Late changes after stencil or fixture preparation has begun
Design maturity issues are the most common source of prototype delays. The plan should require design freeze gates before prototype, pilot, and ramp builds.
2. Component Availability and Lifecycle Risk
- Sole-source or single-source parts
- Long lead times
- Parts near end-of-life
- Moisture sensitivity level issues
- Counterfeit or gray-market component risk
- Incomplete approved vendor list
Each bill of materials should be reviewed for lifecycle status and alternate sources. A component that is available for prototype may not be available for pilot production.
3. PCBA Manufacturability Risk
- Footprint errors
- Insufficient pad spacing
- Poor thermal relief
- Mixed SMT and through-hole assembly constraints
- Fine-pitch and BGA placement challenges
- Panelization and breakaway concerns
- Stencil aperture issues
- Reflow profile limitations
These risks are best addressed through a design for manufacturability review before the first build. A PCBA new product introduction service provider can provide this feedback using actual assembly data.
4. Testability Risk
- Insufficient test points
- Lack of boundary scan access
- Inadequate functional test coverage
- Programming or bootloader access problems
- No clear pass/fail criteria
- Test fixture not ready before pilot
Test gaps allow defects to move from prototype to production. The risk plan should require test coverage review before pilot run.
5. Firmware and Configuration Risk
- Firmware version mismatch
- Unlocked security settings during prototype
- Configuration file errors
- Incomplete bootloader or programming instructions
- No controlled method for firmware updates during manufacturing
Firmware issues often appear only at final test. The risk plan should include firmware release controls as part of the build kit.
6. Supply Chain and Tooling Risk
- PCB fabrication delays
- Stencil or fixture lead time
- Solder paste or material availability
- Assembly capacity conflicts
- Shipping and handling damage
Tooling and material readiness should be confirmed before each NPI build. A delay in a stencil or test fixture can shift the entire schedule.
7. Process Capability Risk
- Solder paste printing repeatability
- Placement accuracy for fine-pitch parts
- Reflow oven profiling
- Selective soldering or wave soldering defects
- Conformal coating or cleaning issues
Process risks should be evaluated during pilot production using production-like tooling and process parameters.
8. Quality and Regulatory Risk
- Acceptance standards not defined
- Missing inspection criteria
- Environmental compliance documentation
- Labeling or traceability requirements
- Product safety or certification requirements
These risks affect final release and should be included early in the plan.
Risk Assessment Method
A simple scoring method works well for electronics NPI. Use a 5×5 matrix for likelihood and impact, and add a detection score if you want a risk priority number.
Example scoring
- Likelihood: 1 = rare, 5 = almost certain
- Impact: 1 = minor schedule delay, 5 = safety, regulatory, or functional failure
- Detection: 1 = easily detected before build, 5 = unlikely to be detected until field use
A useful formula is:
Risk priority = Likelihood × Impact × Detection
This helps prioritize risks that are likely, severe, and hard to detect. For each risk, assign an owner and a target date. Review the register at every NPI phase gate.
Phase-by-Phase Risk Management
Prototype Phase
The prototype build is where design errors become visible. At this stage, the risk plan should focus on:
- Component fit and footprint verification; Basic functional test results; DFM and DFT feedback; Solder joint quality; Programming and firmware access; Mechanical fit and connector alignment;
All issues found during prototype should be logged in the risk register with a corrective action owner.
Pilot Production Phase
The pilot run should use production-like tooling, stencils, fixtures, and test systems. Risks to monitor include:
-
First-pass yield; Solder paste print quality; Placement accuracy for fine-pitch and BGA parts; Test coverage and false failures; Process cycle time; Material traceability; Firmware and configuration stability;
A pilot run is also the time to confirm that the risk controls from prototype have been implemented.
Ramp Phase
During ramp, the risk plan shifts toward supply chain and process stability. Key risks include:
-
Supplier delivery performance; Component substitutions; Process drift; Test equipment capacity; Operator training; Field return data;
The risk register should remain active through ramp and into early production.
Key Technical Controls
A robust NPI risk management plan includes specific technical controls:
Design for Manufacturability and Test Review
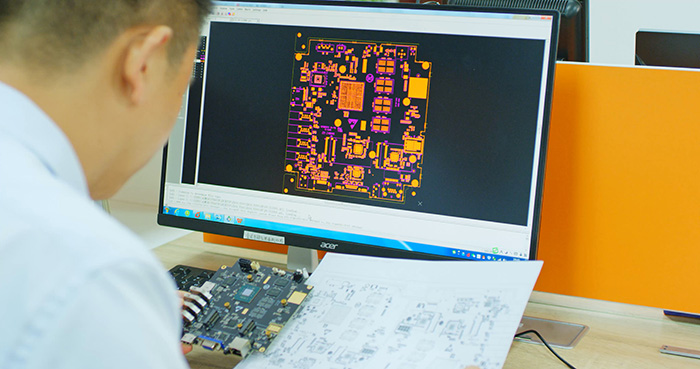
A DFM/DFT review should be completed before the first PCBA build. The review checks pad geometry, component spacing, thermal relief, polarity marking, test access, and panel design. This review converts late-stage assembly issues into early design corrections.
BOM Analysis
A BOM risk analysis should examine every part for availability, lifecycle status, moisture sensitivity, alternate sources, and compliance documentation. Parts with long lead times or sole-source status need mitigation actions.
Process FMEA and Control Plan
A process failure mode and effects analysis identifies where assembly defects are likely to occur. The control plan then defines inspection points, process limits, and response actions.
First Article Inspection
First article inspection verifies that the first assembled boards match the design intent. It covers component placement, polarity, solder joint quality, and dimensional requirements.
Change Control
Any change to the BOM, firmware, stencil, tooling, or test program after a build should trigger a risk review. Uncontrolled changes are a major source of NPI failure.
Documentation and Communication
A risk register is only useful if it is reviewed and updated. The NPI plan should define:
-
Risk register format and fields; Review frequency; Escalation rules; Roles and responsibilities;
A simple RACI matrix can clarify who owns risk identification, who executes mitigation, who approves changes, and who monitors status.
Weekly risk reviews during NPI keep the plan current. Each review should focus on risks that are due, risks that have changed, and risks that need escalation.

How PCBA New Product Introduction Services Support Risk Management
An experienced PCBA manufacturing provider can reduce NPI risk by reviewing the design before the first build, preparing stencils and fixtures, supporting prototype assembly, and collecting process data during pilot production. This allows the risk plan to be based on measured results rather than assumptions.
Shenzhen 1943 Technology Co., Ltd. provides PCBA New Product Introduction Services that include DFM feedback, prototype assembly, test support, and ramp planning. For electronics teams, this type of support helps turn the risk register into a practical build plan, with fewer late-stage board spins and more predictable pilot results.
FAQ
What is an NPI risk management plan in electronics manufacturing?
An NPI risk management plan is a structured document and process for identifying, assessing, and controlling risks during the transition from design to production. In electronics, it typically covers design maturity, component availability, PCBA manufacturability, test access, firmware readiness, supply chain, and ramp stability.
What are the most common risks during PCBA new product introduction?
Common risks include unstable BOMs with long lead or sole-source parts, insufficient test points, footprint errors, solder defects on fine-pitch or BGA packages, firmware version mismatch, late stencil or fixture preparation, and limited pilot-run data.
How do DFM and DFT reviews reduce NPI risk?
Design for manufacturability reviews catch assembly issues such as inadequate spacing, poor thermal relief, or difficult component placement before the first build. Design for test reviews ensure test access and coverage are sufficient. Both convert late-stage discovery into early design corrections, which reduces board spins and schedule delays.
When should an NPI risk management plan be updated?
The plan should be updated at each phase gate: after the prototype build, before the pilot run, after the pilot run, and before ramp. It should also be updated after any significant change in BOM, firmware, tooling, test program, or supplier.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08