PCBA NPI Process: From Design Review to Mass Production
New Product Introduction (NPI) defines the structured workflow that transforms finished PCB design files into stable, repeatable PCBA manufacturing output. Many projects encounter yield drops, schedule delays, or unplanned revisions because functional bench‑tested prototypes are not inherently production‑ready. A standardized PCBA NPI workflow identifies manufacturability, material, and process risks at early stages, avoiding costly modifications after large‑batch manufacturing commences.
1943 Technology delivers PCBA New Product Introduction Services covering the complete workflow from initial design assessment through mass‑production hand‑over. The service aligns engineering, material procurement, assembly, and quality validation to close gaps between laboratory prototypes and factory‑scale production, supporting customers to launch new hardware products with predictable quality and timeline.
1. Design Package Hand‑over and DFM / DFT Review
The NPI workflow formally begins once the customer submits a complete design package, including Gerber data, centroid files, BOM with manufacturer part numbers, assembly drawings, and defined test specifications.
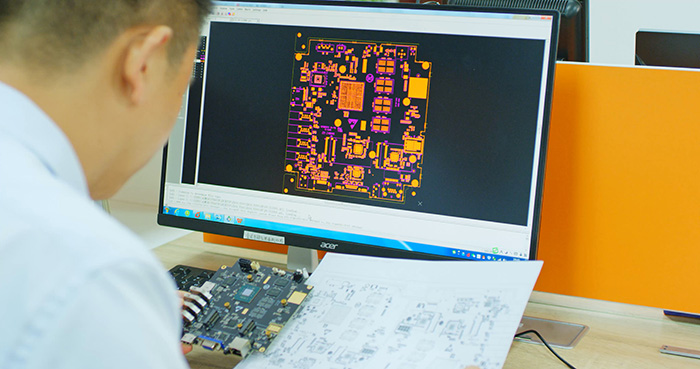
Engineering teams conduct Design for Manufacturability (DFM) and Design for Testability (DFT) assessment rather than relying solely on PCB software DRC outputs. Key review items include component spacing, pad geometry, fiducial placement, panelization schemes, test‑point coverage, and component lifecycle status. Common risks flagged in this phase include inadequate stencil aperture ratios, tombstone‑prone pad layouts, missing local fiducials, and end‑of‑life components listed in BOM.
All identified risks are categorized as critical or advisory. Critical items require design revision before stencil and fixture fabrication. Advisory risks are documented for tracking during first‑article build. The deliverable of this phase is a formal DFM‑DFT report with prioritized optimization recommendations.
2. Material Validation and Pre‑Process Preparation
After design review sign‑off, material validation is performed. Each component entry on the BOM is cross‑checked for availability, packaging compatibility with SMT equipment, and alternative‑part feasibility. Component lead‑time risks are documented so customers can adjust bill‑of‑materials or project timelines accordingly.
Parallel engineering work includes stencil construction, fixture planning, SMT machine programming, and reflow profile development matched to PCB substrate and component thermal characteristics. Test workflows for ICT and FCT are defined, and required test fixtures are scheduled for fabrication. This phase prevents interruptions during physical assembly caused by missing tooling or incompatible component packaging.
3. First‑Article Build and Validation
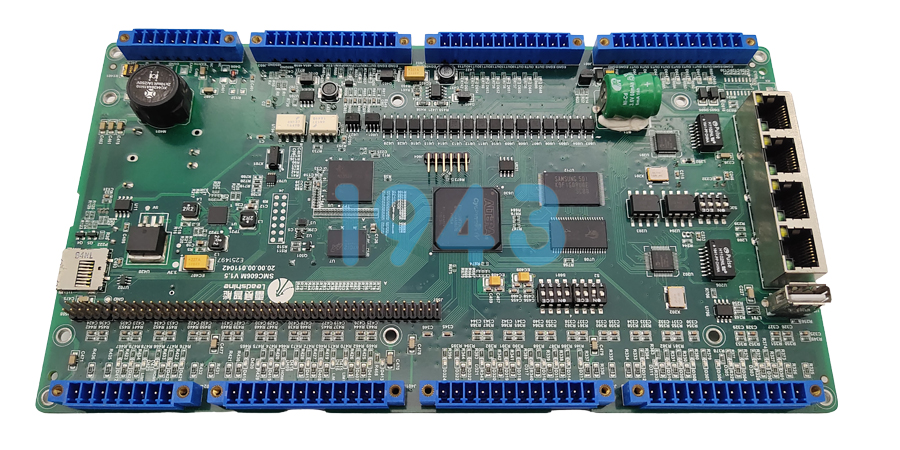
First‑article production executes assembly using finalized stencil, program parameters and test fixtures. The output undergoes multi‑layer inspection: SPI for solder paste deposition, AOI for component placement quality, X‑ray inspection for hidden solder joints of BGA and QFN devices, followed by in‑circuit and functional testing.
Every defect is logged with root‑cause analysis. Issues may stem from layout limitations, stencil design, machine parameter settings, or component physical characteristics. Adjustments are implemented iteratively until the first‑article meets the defined acceptance criteria aligned with IPC‑A‑610 standards. A formal first‑article inspection report is generated for project sign‑off. It is important to note that passing first‑article validation does not equal mass‑production readiness; it only confirms the product can be assembled under controlled laboratory‑like conditions.
4. Pilot Production Run
Pilot production acts as a full‑scale process rehearsal under real factory operating conditions, with standard operators, production‑line workflows, and official tooling. Batch sizes are determined by product complexity, generally ranging from 50 to 500 units.
This stage verifies process repeatability rather than individual board functionality. Engineers track first‑pass yield, categorize defects via Pareto analysis, and document issues related to material feeding, fixture tolerance, assembly sequence, or operator work instructions. Problems rarely visible in single‑unit first‑article builds often emerge during pilot batches. All non‑conformances go through corrective‑action workflows with clear closure criteria.
Upon successful pilot completion, core manufacturing documents are finalized: standard operating procedures, inspection checklists, test protocols, and full traceability requirements. These documents form the baseline for subsequent mass‑production operations. 1943 Technology’s PCBA New Product Introduction Services includes dedicated process‑engineering support throughout pilot runs, compiling complete pilot‑run assessment records for hand‑over.
5. Mass‑Production Release and Knowledge Hand‑over
Mass‑production release occurs only after pilot‑run yield targets are achieved and all identified non‑conformances are closed. The NPI team transfers stabilized processes, complete documentation sets, and historical defect data to serial‑production teams.
Key deliverables handed over to production include validated SOPs, approved reflow profiles, fixture specification sheets, test‑program versions, BOM revision status, and historical failure‑mode records. Traceability rules are locked in place for component lots and production batches.
NPI activities do not fully conclude at release. Short‑term yield monitoring continues for early production batches. Any new recurring defects trigger fast‑track engineering reviews to prevent yield decay as manufacturing volumes expand.
6. Common Transition Risks in PCBA NPI
Many hardware projects face setbacks caused by skipping NPI gate reviews. Typical risks include:
- Assuming a working prototype equals production‑ready design; prototype builds often adopt manual processes that cannot scale to high‑speed SMT lines.
- Unresolved DFM risks carried forward, generating consistent assembly defects in volume batches.
- Unverified component substitutions leading to intermittent functional failures.
- Incomplete documentation, creating inconsistent execution between different production shifts.
Risks identified early in NPI require lower modification cost compared with corrections applied after mass‑production starts.

Frequently Asked Questions
Q1: When should PCBA NPI officially start for a hardware project?
NPI should commence after customers release a controlled, complete design package, rather than immediately after prototype bench validation. A functional prototype only proves design logic, while NPI validates manufacturability, material stability, process repeatability and test workflows. Starting NPI too late increases the probability of expensive redesigns during later project phases.
Q2: What is the core difference between prototype build and NPI pilot production?
Prototype builds prioritize verifying circuit functionality and mechanical fit, often using semi‑manual assembly workflows. NPI pilot production runs under full production‑line conditions. It validates repeatable yield, operator workflows, fixture performance, material feeding behavior, formal inspection and traceability mechanisms. Even if prototypes work perfectly, pilot batches may reveal process‑related defects unseen in small manual builds.
Q3: What documents should I expect upon successful NPI completion?
Standard deliverables include DFM‑DFT review report, first‑article inspection records, pilot‑run yield analysis and defect Pareto report, finalized BOM revision, assembly SOP documents, test specifications, fixture documentation, and closed corrective‑action records for all identified non‑conformances. Complete documentation is essential for stable long‑term serial manufacturing.
Q4: Can NPI work be partially skipped to shorten project lead‑time?
Skipping or compressing NPI gate reviews may reduce short‑term timeline, yet it frequently introduces hidden risks. Unvalidated processes may trigger low yield, unexpected rework, field unit failures, and overall longer total project cycles. Where tight deadlines exist, the recommended approach is parallel processing of DFM review and material preparation, rather than omitting validation stages.
Conclusion
The PCBA NPI process connects design engineering to stable manufacturing through sequential gate‑checked stages: design review, material validation, first‑article verification, pilot production, and mass‑production hand‑over. Each phase targets specific risk categories to prevent avoidable yield loss and schedule disruption.
1943 Technology’s PCBA New Product Introduction Services implement this phased methodology, helping customers bridge from prototype validation to mature serial manufacturing. Thorough NPI execution establishes stable process baselines, reduces revision frequency, and creates clear documentation foundations for the full product lifecycle.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08