What Is Included in PCBA Pilot Run NPI Service
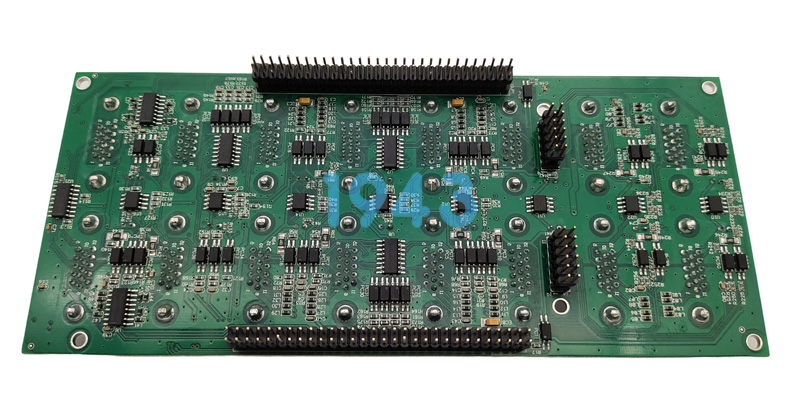
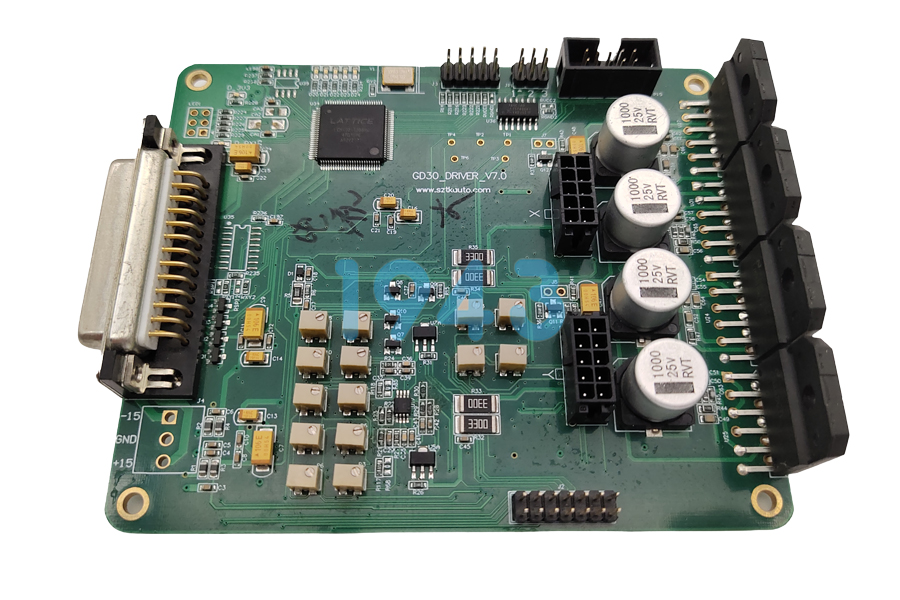
For OEMs and electronics brands, moving a new printed circuit board assembly from design validation to mass production is one of the most risk-dense phases in the entire product lifecycle. The PCBA pilot run—often referred to as NPI pilot production—is the first time your design meets actual manufacturing conditions. What happens during this stage determines whether your product launches on schedule, meets yield targets, and avoids costly re-spins.
This article breaks down exactly what is included in a professional PCBA pilot run NPI service, with practical details for engineering and operations teams evaluating contract manufacturing partners.
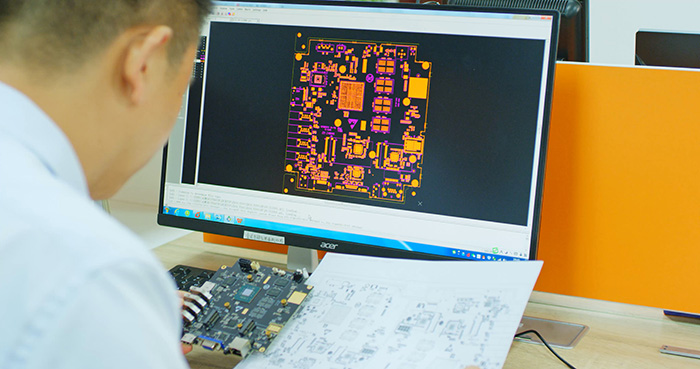
1. Design for Manufacturing Review
Before any board enters the SMT line, the NPI service begins with a structured DFM analysis. This is not a superficial checklist. It examines:
- Pad and land pattern dimensions against component specifications
- Solder mask openings and alignment tolerances
- Component placement clearances (mechanical and thermal)
- Test point accessibility for ICT and flying probe
- Fiducial mark placement and board edge clearances
- Panelization layout for assembly and depaneling
The goal is to identify potential soldering defects, tombstoning risks, and assembly bottlenecks before steel stencils are cut. A thorough DFM review typically returns 15–30 actionable recommendations per design, with severity rankings that help your engineering team prioritize changes.
2. Bill of Materials Verification and Sourcing
The BOM provided during design phase often differs from what is actually available or manufacturable. NPI pilot service includes:
- Component lifecycle status review – identifying end-of-life or NRND parts
- Alternate component qualification – form-fit-function replacements with documented comparisons
- Supply chain risk assessment – single-source vs. multi-source components
- Lead time validation against pilot schedule
- Moisture sensitivity level classification and baking requirements
For pilot runs, the NPI team procures prototype quantities (typically 50–200 assemblies) while verifying that all parts meet the specified tolerances. Any deviations are documented and presented with engineering change recommendations.
3. Stencil Design and Fabrication
The solder paste printing process accounts for over 60% of soldering defects in surface-mount assembly. NPI service includes stencil design optimization:
- Aperture geometry adjusted for specific component types (fine-pitch QFNs, BGAs, 0201 passives)
- Step stencil considerations for boards with mixed component heights
- Electro-polishing for cleaner paste release
- Framed or frameless options based on your printer equipment
Stencil fabrication is coordinated to arrive with components, ensuring the assembly line is not waiting on tooling.
4. SMT Program Development and Optimization
Each PCBA pilot run requires new pick-and-place programs. This includes:
- Component database creation with correct feeder types, nozzle sizes, and placement speeds
- Mounting sequence optimization to balance head movement and reduce cycle time
- Vision alignment settings tailored to component body and lead configurations
- Feeder assignment planning for efficient material kitting
The NPI team runs program simulations before loading actual boards. First-pass placement accuracy is verified using test coupons or glass plates before production starts.
5. First Article Inspection
First article inspection is the formal documentation process that captures every critical dimension and assembly characteristic from the first assembled board. The FAIR package includes:
- Dimensional measurements per IPC-6012 and customer drawings
- Solder joint inspection (wetting angle, fill, fillet shape)
- Component placement accuracy verification
- X-ray inspection for BGA, QFN, and LGA solder joints
- Cross-section analysis when specified
- Tape-and-reel component verification against BOM
Each measurement is recorded against specified tolerances, with deviations flagged for engineering disposition. The FAIR is typically submitted for customer approval before moving to the full pilot batch.
6. In-Circuit and Functional Testing
Pilot run NPI service includes test fixture development and validation:
- ICT fixture design and fabrication for beds-of-nails access
- Flying probe programming for low-volume pilot validation
- Functional test fixture development tailored to your product specifications
- Boundary scan test development for JTAG-enabled boards
- Test coverage analysis showing which nodes are accessible and which require functional validation
The test development runs in parallel with assembly so that test fixtures are ready by the time first assemblies come off the line.
7. Process Capability Documentation
For each pilot run, the manufacturing team records critical process parameters:
- Reflow profiles (temperature curve, soak time, time above liquidus)
- Solder paste inspection data (volume, area, height)
- Placement accuracy statistics per component type
- Yield breakdown by defect category
- Cycle time measurements per operation
This data package is delivered with the pilot shipment and becomes the baseline for mass production process control.
8. Rework and Failure Analysis Support
Pilot runs inevitably reveal issues. Professional NPI service includes:
- On-site rework capability for engineering change implementation
- Failure mode analysis for any functional failures
- Corrective action tracking with documented verification
- Component removal and replacement for design modifications
The NPI team maintains rework logs showing what was changed, why, and how it was validated.
9. Final Assembly and Packaging
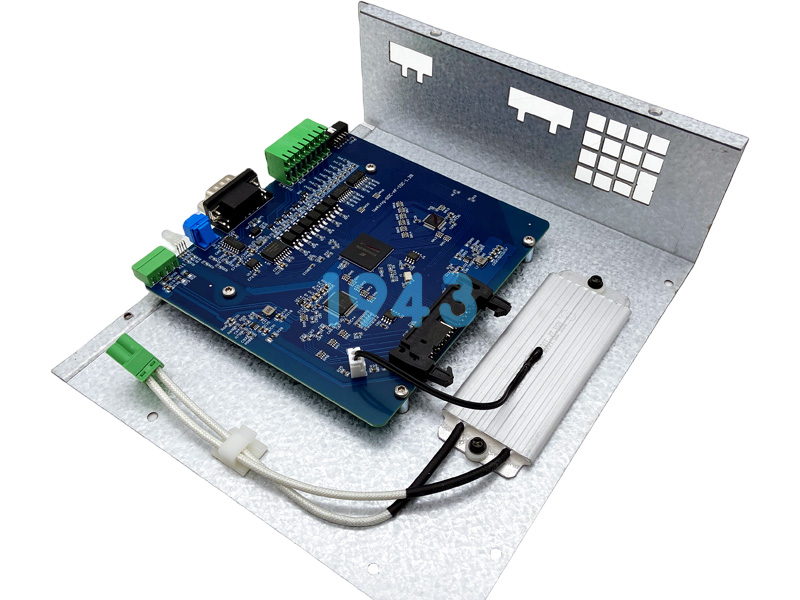
For complete PCBA pilot assemblies, the service extends to:
- Conformal coating application when specified
- Underfill for BGA reliability
- Selective soldering for through-hole components
- Wash and cleanliness testing for no-clean or water-wash processes
- ESD-safe packaging with moisture barrier bags and humidity indicators
- Labeling with assembly revision, date code, and serialization
10. Handoff Documentation
The pilot run concludes with a comprehensive data handoff that enables your team to release the product for volume production:
- Fully documented assembly process specifications
- Qualified component substitutes list
- Test program files and fixture drawings
- Yield and defect Pareto charts
- Risk assessment for remaining unresolved issues
- Recommended inspection criteria for incoming QC
Why the Pilot Run Matters
The PCBA pilot run is not a formality—it is the only opportunity to validate your manufacturing process before committing to production volumes. A properly executed NPI service reduces the risk of field failures, improves first-pass yield, and shortens the overall time from prototype to market.
1943 Technology’s PCBA New Product Introduction Services are structured around the specific challenges of bringing complex assemblies through the pilot phase. Our engineering team works directly with your design and operations groups to ensure every parameter is documented, every risk is assessed, and every process is ready for scale.

Frequently Asked Questions
Q1: What is the typical quantity for a PCBA pilot run?
Pilot run quantities typically range from 50 to 200 assembled boards, depending on the product complexity and production volume targets. Some customers run as few as 20 boards for high-value systems or as many as 500 for simpler assemblies. The pilot quantity is determined by the amount of material needed to validate process capability—typically enough to generate statistically meaningful yield data while minimizing waste if design changes are required.
Q2: How long does a PCBA pilot run NPI cycle take?
The NPI cycle from DFM review to completed handoff typically takes 10 to 20 working days, depending on component lead times and the complexity of test fixture development. Simple assemblies with standard components and minimal test requirements can complete in 7–10 days. Complex boards with custom BGAs, multiple test stages, and extensive FAIR documentation may require 4 weeks or more. The timeline is established during project kick-off and updated weekly.
Q3: What is the difference between a prototype build and a pilot run?
Prototype builds are conducted during the design phase to verify function and form. Pilot runs occur after design sign-off and are performed on production-equivalent equipment with production-ready tooling and processes. The pilot run validates that the manufacturing process can consistently produce assemblies that meet specifications. Prototypes focus on "does it work," while pilot runs focus on "can we manufacture it reliably."
Q4: What happens if a defect is found during the pilot run?
Defects identified during pilot run are documented through a formal corrective action process. The NPI team isolates the root cause—whether it is design-related, material-related, or process-related—and implements a corrective action. The affected assemblies are reworked or scrapped as appropriate, and the corrective action is verified on subsequent assemblies. A full report is provided to the customer with recommendations for preventing recurrence in volume production. No pilot assembly is shipped without documented resolution of any critical issues.
For detailed engineering consultation on your specific PCBA pilot requirements, contact 1943 Technology's NPI engineering team with your design package for a comprehensive capability review.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08