Relationship Between PCBA NPI Service and Low‑volume Pilot Production
Why NPI and Pilot Production Must Be Planned Together
In PCBA manufacturing, the gap between a validated prototype and a stable production line is where most hardware projects lose time and budget. New Product Introduction (NPI) is the structured engineering process that closes this gap. Low‑volume pilot production is the physical proof that the process holds. Neither works in isolation. Treating them as separate phases—one handled by the design house, the other handed to a contract manufacturer—creates information loss, rework loops, and schedule slips.
This article breaks down how a disciplined PCBA NPI service connects directly to pilot‑run execution, what deliverables each stage produces, and what engineering teams should verify before committing to volume output.
What PCBA NPI Actually Covers
NPI is not a single gate review. It is a sequence of engineering activities that starts after schematic and layout freeze and ends when the assembly process is capable of running at target yield without constant intervention.
Core NPI activities include:
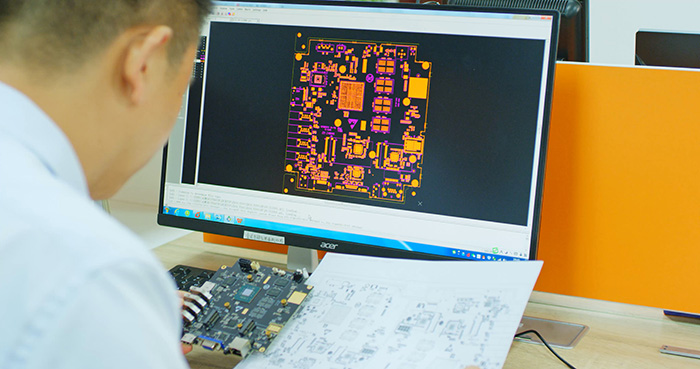
- Design‑for‑Manufacturing (DFM) and Design‑for‑Test (DFT) review. Checking pad geometry, solder mask clearances, fiducial placement, component keep‑out zones, panel utilization, and test‑point accessibility before any board is fabricated.
- Bill of Materials (BOM) validation. Confirming every part number is active, has a qualified second source, and matches the footprint on the PCB data. Flagging end‑of‑life or long‑lead‑time components early.
- Process routing definition. Selecting solder paste alloy, stencil aperture design, reflow profile parameters, wave or selective soldering requirements, and cleaning specifications based on the board's actual component mix.
- Fixture and tooling planning. Identifying ICT, FCT, or boundary‑scan fixtures; designing assembly jigs for odd‑form or hand‑loaded parts.
- Risk register and mitigation plan. Documenting every known process risk—warpage on thin boards, fine‑pitch BGA alignment, mixed‑technology soldering—and assigning corrective actions with owners.
At 1943 Technology, these activities are bundled into a single PCBA New Product Introduction Services engagement, so the same engineering team that performs the DFM review also owns the pilot‑run process sign‑off. This eliminates the handoff gap that typically appears when design review and production planning sit in different organizations.
What Low‑volume Pilot Production Is—and What It Is Not
A pilot run of 20 to 200 boards is not a small batch of mass production. Its purpose is to generate process data, not to ship sellable units.
Specific goals of a pilot build:
- Verify the reflow profile against actual board mass, copper distribution, and component thermal loads. Record peak temperature, time above liquidus, and cooling slope for each zone.
- Confirm stencil print quality. Measure paste volume, offset, and release behavior on the smallest aperture in the design.
- Validate placement accuracy for components at 0.4 mm pitch or below, and for any package with a thermal pad or exposed die attach.
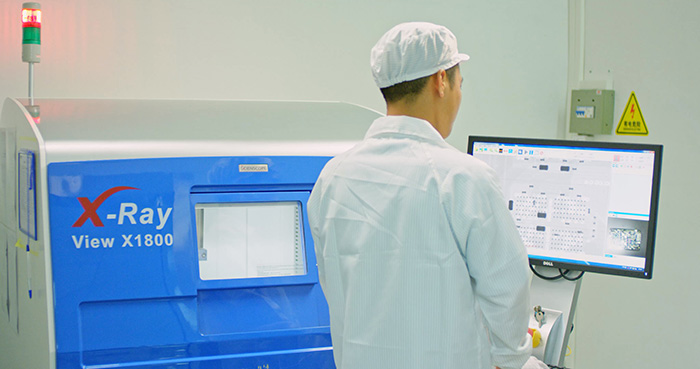
- Run the full test sequence—ICT, flying probe, or functional test—to confirm coverage targets and identify any DFT gaps that were missed in the NPI review.
- Document first‑pass yield and defect Pareto. Classify every defect (tombstone, solder bridge, lifted pad, void) and trace it to a root cause before the next build.
If the pilot run is skipped or compressed, these data points surface for the first time during volume production, where the cost of correction is an order of magnitude higher.
How NPI Feeds Directly into Pilot Execution
The relationship is sequential and data‑dependent:
| NPI Output | Pilot‑Run Input |
|---|---|
| DFM/DFT report with corrective actions | Revised Gerber and drill files loaded into CAM |
| Approved BOM with AVL (Approved Vendor List) | Kitted materials pulled from qualified suppliers |
| Process routing sheet | Machine programs written for printer, pick‑and‑place, reflow |
| Stencil aperture spec | Laser‑cut or electroformed stencil fabricated and inspected |
| Test plan and fixture design | ICT/FCT fixtures built, debugged, and calibrated |
| Risk register | Inspection checklist for each critical station |
If any row in this table is incomplete or outdated, the pilot run generates noise instead of signal. Boards fail for reasons unrelated to the actual design, and the team wastes a build cycle chasing process artifacts.
A structured NPI service ensures every row is closed before the first panel enters the SMT line. 1943 Technology's PCBA New Product Introduction Services assign a dedicated process engineer to walk through this checklist with the customer's hardware team before the pilot order is released to the shop floor.
Key Process Windows to Lock Down During Pilot
Solder Paste and Stencil
For boards mixing 0201 passives with 0.5 mm pitch BGAs, a single stencil thickness rarely works. Step‑up or step‑down regions, or a dual‑print approach, may be required. The pilot run is where you confirm aperture volume delivers between 80 % and 120 % of the theoretical paste deposit for each pad type.
Reflow Profile
Thermocouple placement must represent the heaviest thermal mass and the lightest component on the same board. A profile that satisfies the largest ground‑plane BGA may overheat a small QFN on the board edge. Record profiles for at least three board positions.
Inspection and Test
AOI programming should be finalized during the pilot, not during volume ramp. Use the pilot boards to build the defect library, set sensitivity thresholds, and confirm false‑call rates stay below 2 %. Functional test scripts should execute the full power‑on sequence, communication protocol checks, and any firmware version validation.
Transition Criteria: From Pilot to Volume
A pilot run is complete when the following conditions are met simultaneously:
- First‑pass yield ≥ 95 % across two consecutive builds.
- No open defect categories with occurrence rate above 1 %.
- All test fixtures passing GR&R (Gauge Repeatability & Reproducibility) within 10 %.
- BOM fully sourced with confirmed lead times for volume quantities.
- Process FMEA reviewed and all high‑RPN items addressed.
- Customer engineering sign‑off on golden sample boards.
Until every criterion is closed, scaling to 500 or 5,000 units per month introduces uncontrolled variables. A disciplined NPI provider will hold the volume release gate until the data supports it.
Common Mistakes That Break the NPI‑to‑Pilot Link
- Starting component procurement before DFM closure. A part substitution after layout freeze can change pad geometry, stencil aperture, and reflow thermal behavior, invalidating earlier process work.
- Running the pilot on a different line or factory than volume production. Machine calibration, conveyor width, and oven zone count differ between lines. Data from one setup does not transfer cleanly to another.
- Skipping DFT review. Without adequate test points and access for probes, the pilot cannot generate meaningful electrical coverage data, and defects ship undetected.
- Compressing the timeline. A five‑day turnaround on a 150‑board pilot leaves no time for two reflow profile iterations or a stencil re‑cut. The result is a "pilot" that proves nothing.
How 1943 Technology Structures the Workflow
1943 Technology operates its PCBA New Product Introduction Services as a fixed‑scope engineering engagement preceding any production order. The sequence is:
- Week 1 – Data intake and DFM/DFT review. Customer provides Gerber, BOM, pick‑and‑place file, and test requirements. Engineering returns a written report with categorized findings (critical / major / minor).
- Week 2 – Process routing and tooling release. Stencil, fixtures, and machine programs are prepared. Long‑lead components are ordered against the approved BOM.
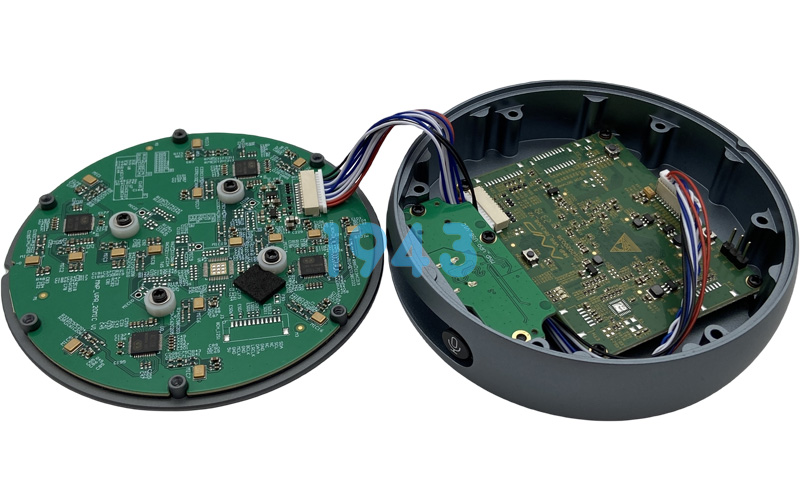
- Week 3 – Pilot build (typically 50–200 units). Boards run through SMT, THT (if applicable), cleaning, inspection, and test. All process parameters are logged per board serial number.
- Week 4 – Data review and corrective action. Yield report, defect Pareto, and process capability data (Cpk for critical dimensions) are delivered. Any open items get a closure plan with target dates.
- Release gate. Volume production order is accepted only after the customer approves the pilot data package.
This structure keeps the NPI engineering team and the production operators working from the same data set, reducing the iteration count between design intent and stable output.

Frequently Asked Questions
Q1: How many boards should a PCBA pilot run include?
A: For most board assemblies, 50 to 200 units provide enough sample size to identify recurring process defects and generate statistically meaningful yield data. Fewer than 20 boards rarely surface intermittent issues such as marginal paste release or borderline reflow windows. The exact quantity depends on the number of unique component packages and the complexity of the test sequence.
Q2: Can we skip the pilot run and go straight to volume production if the prototype worked?
A: Prototype boards are typically hand‑assembled or built on a development line with different equipment, solder paste, and operator technique. Volume SMT lines run at higher placement speeds, use different conveyor thermal profiles, and rely on automated optical inspection rather than manual visual checks. Skipping the pilot means the first volume run becomes the experiment, and defect costs scale with quantity.
Q3: What files and documents does a PCBA NPI service need to start?
A: At minimum: fabrication Gerber and drill files, IPC‑2581 or ODB++ database, approved BOM with manufacturer part numbers, centroid/pick‑and‑place file, assembly drawings, test specifications (ICT coverage targets, functional test scripts), and any known compliance requirements (IPC‑A‑610 class, cleanliness standard). Providing these in a single package at project start avoids multiple clarification cycles.
Q4: How long does a typical NPI‑to‑pilot cycle take at 1943 Technology?
A: For a standard board with up to 400 unique component lines and no exotic substrates, the cycle from data intake to pilot data delivery is three to four weeks. Boards with HDI structures, press‑fit connectors, or conformal coating requirements may add one to two additional weeks for tooling and process qualification. Timelines are confirmed in writing before the engagement begins.
Final Note
The value of a PCBA NPI service is measured not by how quickly it produces boards, but by how few surprises remain when the volume order starts. Low‑volume pilot production is the mechanism that converts engineering assumptions into measured process data. Linking the two under one engineering ownership—design review, process planning, pilot execution, and data closure—shortens the overall program timeline and reduces the total cost of introduction.
For teams preparing a new board design for manufacturing, the first practical step is a structured DFM/DFT review against the actual production process. 1943 Technology's PCBA New Product Introduction Services begin at exactly that point, and carry the project through pilot validation to a controlled volume release.
Latest information
Let the products quickly and stably realize marketization and become the global electronic intelligence innovation enabler

 2026-09-08